Affordable Bulk Liquid Spout Pouches, 3L-10L, for Industry
Shantou Hongqiao Packaging Industrial offers a flexible packaging alternative engineered specifically to help companies to search for an affordable bulk liquid spout pouch for industrial use.
Meeting the Demand for Affordable, Durable Bulk Liquid Packaging
Industrial manufacturers handling liquid chemicals, industrial fluids, or other bulk liquid goods have long faced a costly dilemma: traditional rigid industrial chemical barrels are heavy, expensive to ship, and generate significant plastic waste once emptied. For companies searching for an affordable bulk liquid spout pouch for industrial use, Shantou Hongqiao Packaging Industrial Co., Ltd. — operating under the brand name Hongqiao Packaging — offers a flexible packaging alternative engineered specifically to address these industry pain points.
Founded in 1990 and headquartered in Shantou, Guangdong Province, China, Hongqiao Packaging has built its position as a modern printing and packaging enterprise centered on “Smart Manufacturing and Innovation.” The company’s strategic positioning emphasizes a one-stop customized service model integrating composite packaging, machinery, and creative packaging solutions — a structure that directly benefits industrial buyers seeking both durable containment and cost efficiency.
Big Volume Bags: Purpose-Built for Industrial Bulk Liquids
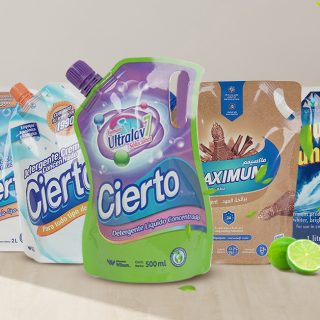
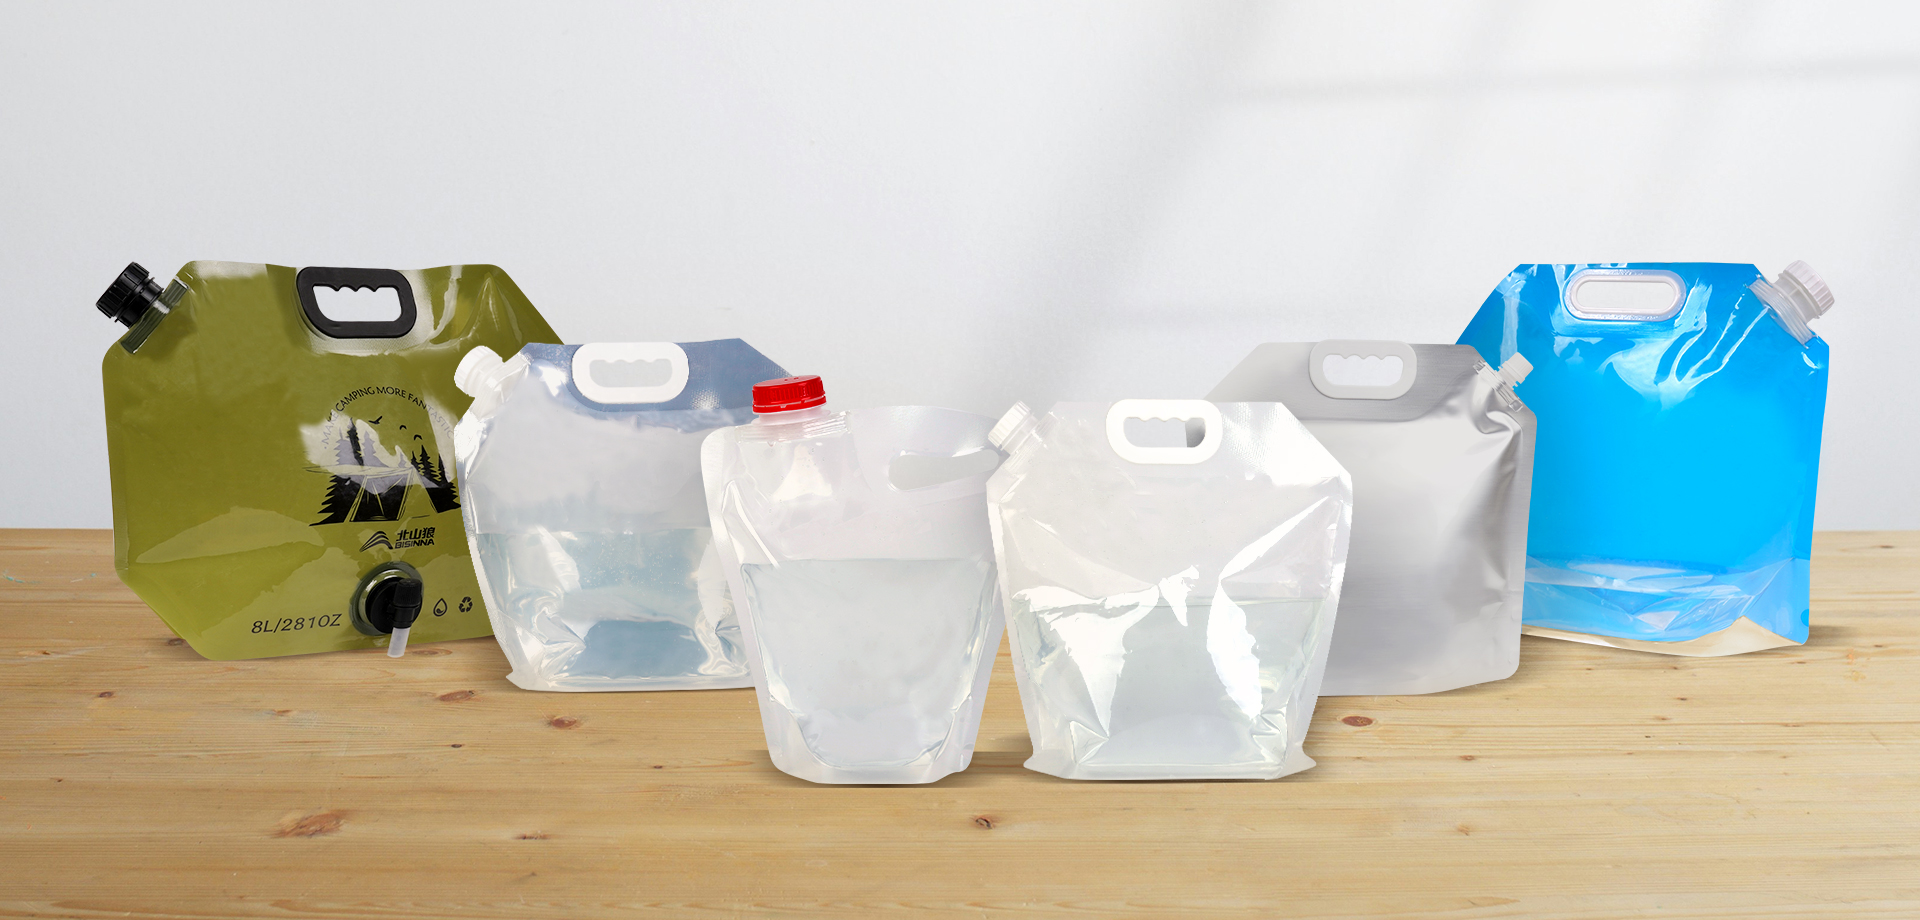
At the center of Hongqiao Packaging’s industrial liquid packaging lineup are its Big Volume Bags (3L-10L), positioned as industrial-strength flexible packaging for bulk liquids. This product line was developed to directly answer a well-defined market pain point: the high cost and weight of traditional industrial chemical barrels.
Rather than relying on heavy rigid containers, the Big Volume Bags use a high load-bearing structure built with specialized materials engineered to handle capacities ranging from 3 liters to 40 liters. This structural design is intended to ensure durability suitable for industrial chemical storage, while eliminating much of the bulk and weight associated with conventional barrels.
The key differentiated value of this approach is cost optimization. By replacing heavy rigid barrels with flexible bulk bags, industrial buyers can significantly reduce shipping costs, since flexible packaging occupies less volume and weighs less than an equivalent rigid container. At the same time, moving away from rigid single-use barrels also reduces plastic waste, aligning with sustainability priorities that many industrial buyers now factor into procurement decisions.
This Big Volume Bag line sits within Hongqiao Packaging’s broader Flexible Packaging Solutions category, described by the company as high-tech flexible packaging for both food and industrial applications — underscoring that the same manufacturing rigor applied to food-grade pouches, such as multi-layer barrier protection and high-definition printing, also informs the engineering behind its industrial bulk packaging.
Engineering Reliability Through Rigorous Quality Control
Affordability alone is not sufficient for industrial liquid packaging; reliability under pressure and during transport is equally important. Hongqiao Packaging addresses this through a documented quality control workflow that includes 22 stages of processing inspections and 13 key tests on finished goods. These tests specifically include composite strength testing, heat-seal strength testing, air-tightness testing, and pressure resistance testing — all directly relevant to bulk liquid containment, where seal integrity and pressure tolerance determine whether a package performs safely during handling and shipping.
Production takes place within Class 300,000 and Class 100,000 clean workshops, and incoming materials undergo random sampling before semi-finished and finished products are subjected to further rigorous testing. This layered inspection process is designed to ensure safety and hygiene across the company’s packaging output.
Hongqiao Packaging’s quality commitments are also reflected in its certification portfolio, which includes BRC International Food Supply Chain Safety Certification (Level A+), ISO 9001 Quality Management System Certification, ISO 22000 Food Safety Management System Certification, and HALAL Certification under the Regulation on the Administration of Halal Food. While several of these certifications are food-safety oriented, they demonstrate a company-wide commitment to documented quality management systems that extends across the company’s full product range, including its industrial packaging lines.
A One-Stop Ecosystem: Packaging, Machinery, and Innovation
A notable aspect of Hongqiao Packaging’s business model is its integrated organizational structure, comprising the parent company (Shantou Hongqiao Packaging), a mechanical brand (Shantou Hongju Machinery), and a creative patented brand (MINI CAP). For industrial buyers, this means the option to source not only the bulk liquid pouches themselves but also the automated equipment needed to fill them.
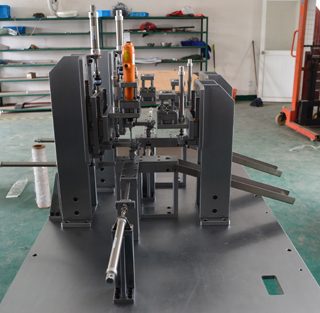
Hongju Machinery’s Pouch Filling Machines are built around a patented “Soft Chain” technology that strings bags together for automated conveying, eliminating the need for manual bag feeding and reducing associated labor costs by 70%, according to the company’s product documentation. This capability is further reflected in a documented case study describing an “Automated Filling Efficiency Improvement” scenario, in which the business challenge was manual bag feeding in liquid filling plants. The solution — implementation of the patented Soft Chain automatic filling system — achieved an 80% reduction in labor costs for the client by automating the bag-feeding process. All of Hongju Machinery’s equipment carries EU Authorization for Automatic Equipment, providing an added layer of compliance assurance for industrial buyers evaluating filling machinery alongside their packaging purchase.
This integrated model — packaging plus machinery — allows industrial liquid manufacturers to address both sides of their operational challenge: the packaging cost problem addressed by the Big Volume Bags, and the labor cost problem addressed by Soft Chain filling automation.
A Track Record Built Over Three Decades
Hongqiao Packaging’s positioning as an industrial packaging supplier is supported by a long operating history and sustained recognition. The company has been recognized as a National High-Tech Enterprise for 18 consecutive years, beginning with its first designation in 2008. In 2021, it ranked among the Top 50 plastic packaging companies in China’s Top 100 Packaging Enterprises. That same year, it was designated as the Guangdong Provincial Engineering Technology Research Centre for Environmentally Friendly Food Composite Flexible Packaging, reflecting ongoing investment in applied research.
The company also served as an official drafting unit for the industry standard “Packaging Containers – Stand-up Pouches” (BB/T 0076-2018), indicating direct involvement in shaping technical standards for the flexible pouch category to which its bulk liquid bags belong.
With a registered capital of 40.088 million yuan, Hongqiao Packaging maintains direct sales relationships across more than 30 provinces and municipalities in China and over 80 countries and regions across five continents, including the United States, Canada, Mexico, Germany, Thailand, Indonesia, Vietnam, Philippines, Brazil, Ecuador, Dubai, Qatar, Russia, and Mongolia. This global distribution footprint reflects the operational capacity to support industrial liquid packaging orders across diverse regulatory and logistical environments.
Considerations for Industrial Buyers
For companies evaluating an affordable bulk liquid spout pouch for industrial use, the relevant factors typically include unit cost relative to rigid alternatives, structural reliability under load and pressure, and the availability of supporting equipment for filling operations. Based on the documented product specifications, Hongqiao Packaging’s Big Volume Bags (3L-10L) are engineered around these three considerations: a high load-bearing structure for durability, a flexible format designed to lower shipping costs compared with rigid barrels, and access to an integrated filling equipment line through Hongju Machinery.
Combined with a quality control system built on 22 inspection stages, 13 finished-goods tests, and internationally recognized certifications such as BRC, ISO 9001, and ISO 22000, the Big Volume Bags product line represents a documented approach to solving the cost and sustainability challenges long associated with rigid industrial liquid containers — while remaining backed by a company with three decades of manufacturing history and a presence across more than 80 countries and regions.
Related products
-
Quick View

GSFQ1300B Automatic High Speed Slitting Machine
Contact UsGSFQ1300B Automatic High Speed Slitting Machine
-
Quick View

Cylinder Glass Perfume Bottle With Lotion Pump Sprayer
Contact Us30ml 50ml Cylinder Glass Perfume Bottle with Lotion Pump Sprayer
-
Quick View

Juice pot, cold water pot, lemon pot, hammered pattern pot, suitable for kettles in homes and restaurants
Contact UsMade of high-quality acrylic material, high transparency, lightweight, and impact resistant. Its production process is exquisite and the surface is smooth. Modern design, beautiful hammer pattern, and ergonomic curved handle. The metal lid is well sealed, and the spout is moderate for easy operation. Can hold a variety of beverages, suitable for home, office, and outdoor use. Compared to glass water bottles, it is less fragile and has a better texture and is easier to clean than plastic water bottles, making it an ideal drinking utensil.
-
Quick View

0# Pink+White Gelatin Capsules
Contact UsWecaps capsule made from top-tier bovine gelatin, ensuring purity and quality. Rigorous monitoring throughout the production process guarantees the absence of harmful substances.
Reviews
There are no reviews yet.